01 Station
Edge buffing
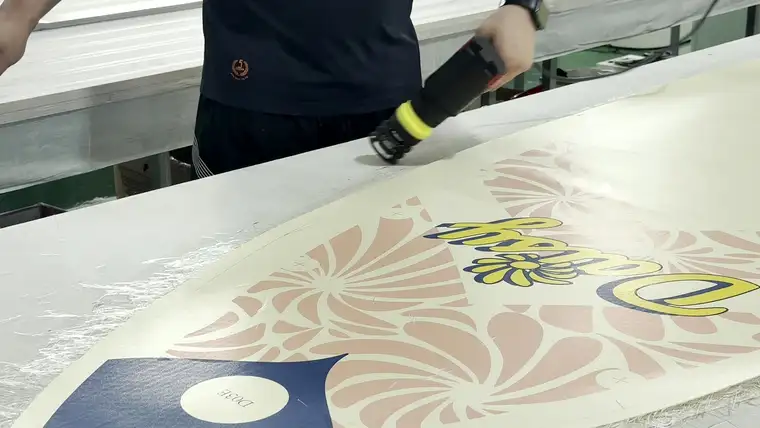
A buffing wheel roughens the airtight edge and the drop-stitch skin so the adhesive keys into the surface.
05Process & QC
A board is glued, welded, pressed and sprayed before it is allowed to rest.
01Holding rules
Time is part of the spec. Every board sits through the same rests, and a batch holds pressure for 48 hours before it is released.
02Main line
01 Station
A buffing wheel roughens the airtight edge and the drop-stitch skin so the adhesive keys into the surface.
02 Station
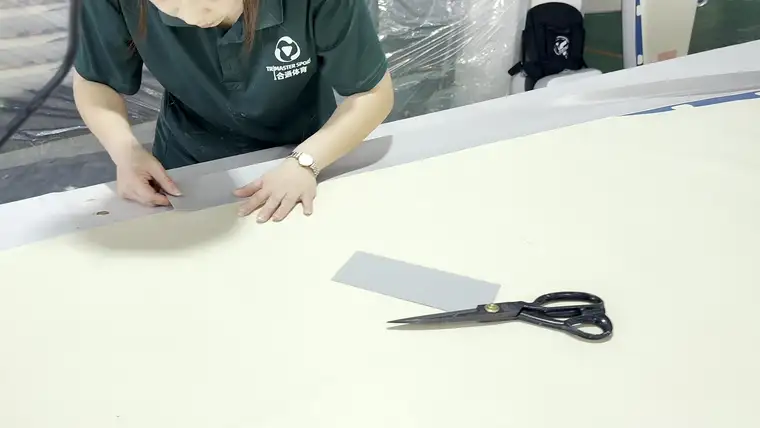
The inner sealing PVC band is measured against the outline of the board and cut to the curve.
03 Station
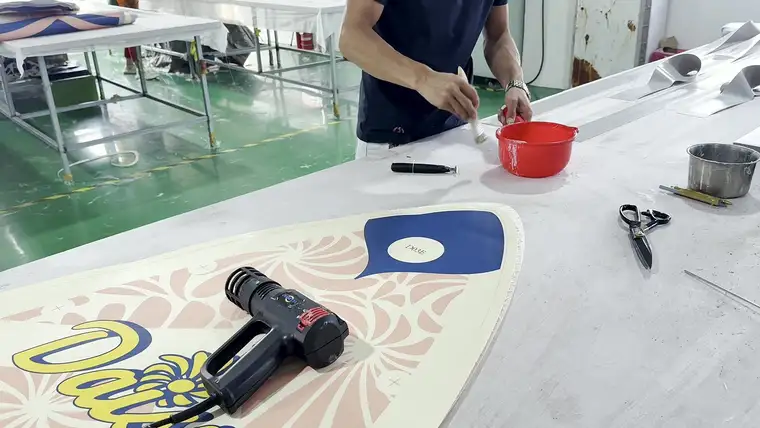
Polyurethane adhesive is brushed on by hand and left to open for a set time before the band goes down.
04 Station
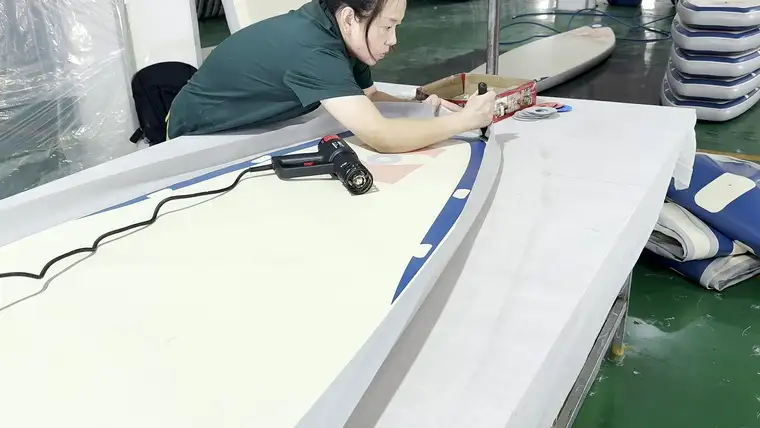
A hot-air gun reactivates the glue and a steel hand plate presses the band down in sections.
05 Station
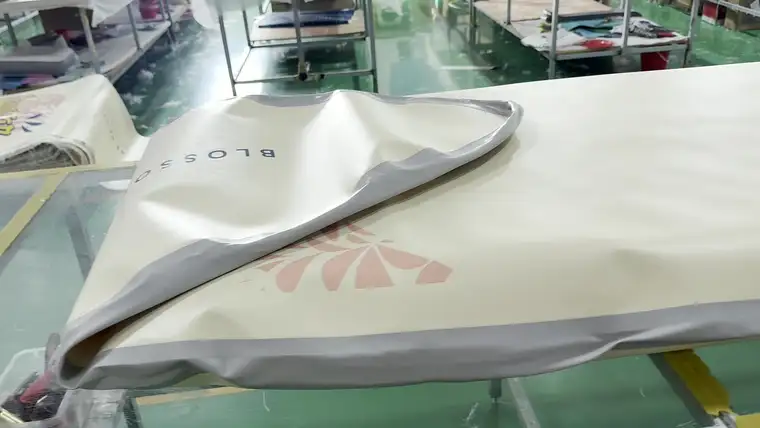
The sealed blank is inflated for the first time so rocker, symmetry and structure can be checked on shape.
06 Station
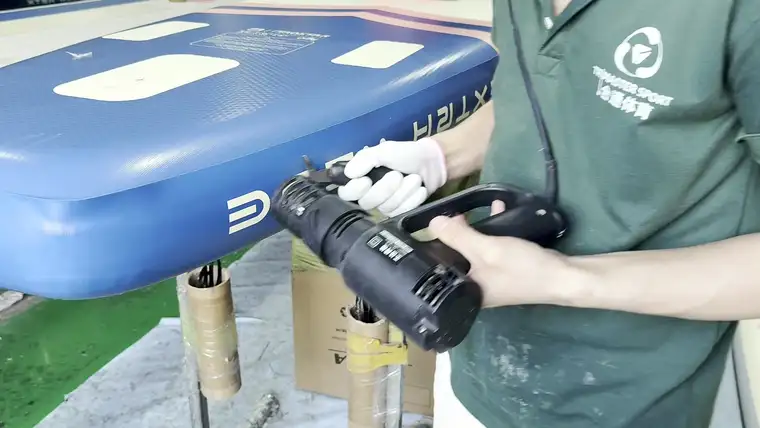
A high-tensile PVC rail goes over the seam and is hot-air welded, which is where the impact and tear margin is added.
07 Station
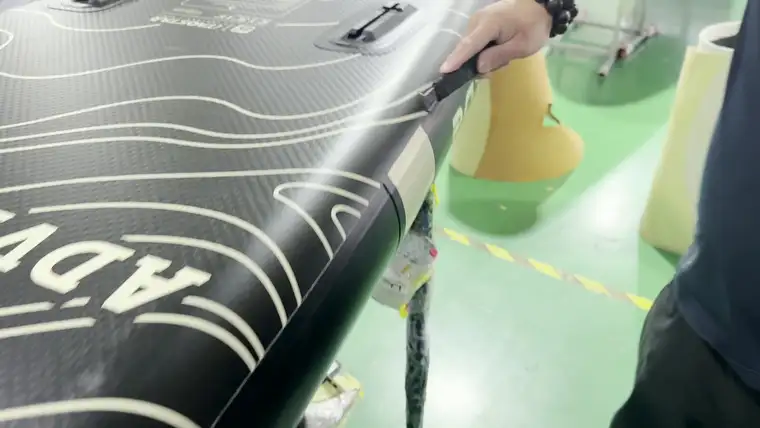
Under pressure, a scraper lifts the overflow glue so the rail line reads clean to the hand.
08 Station
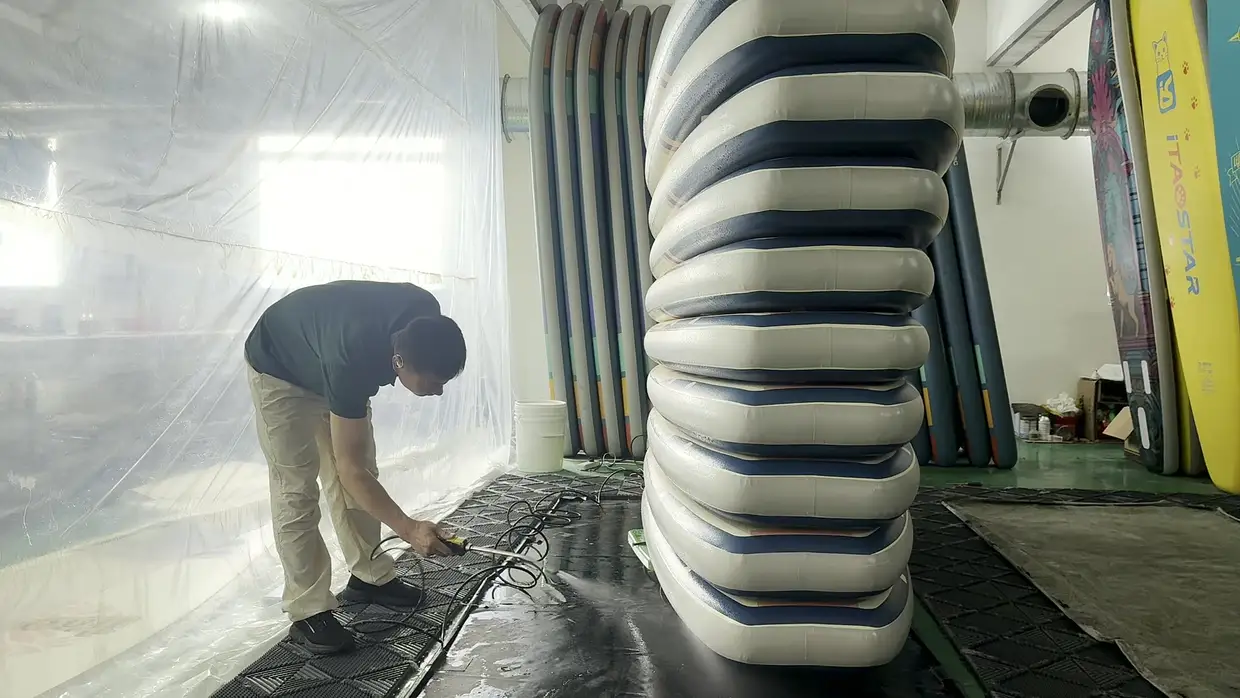
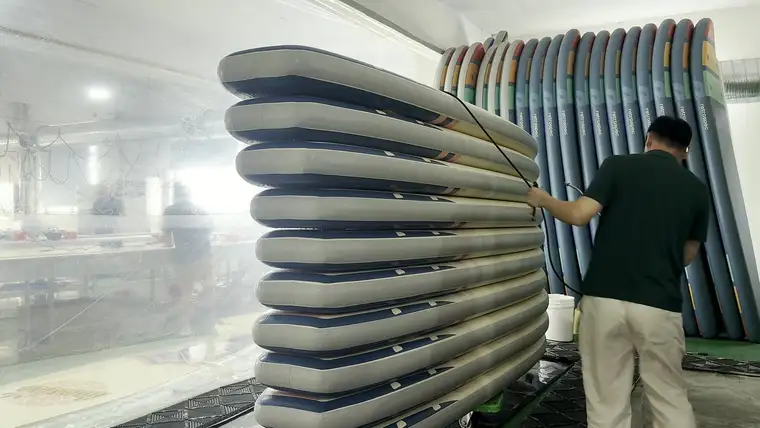
Boards are inflated to working pressure, stacked, and sprayed with water mist seam by seam to read the bubbles.
09 Station
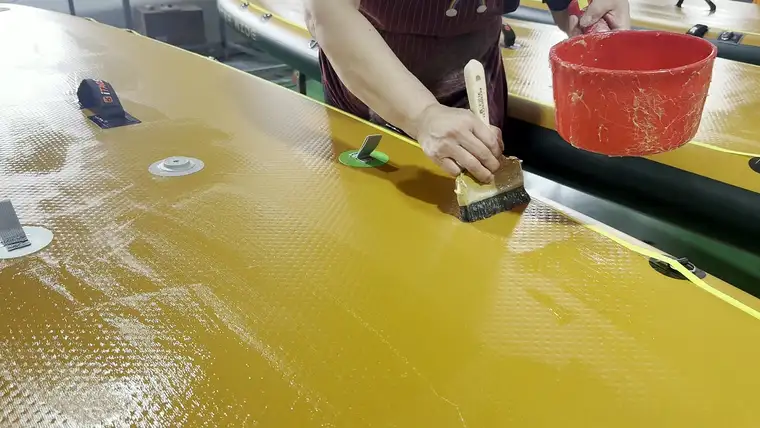
Masking tape holds the pad boundary while a wide brush spreads adhesive clear of the handle and valve bases.
10 Station
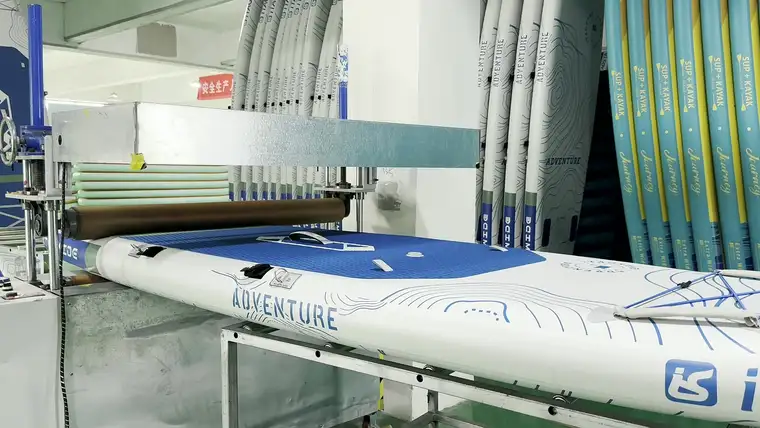
The board runs through a roller line under constant pressure, which drives out the last trapped air.
11 Station
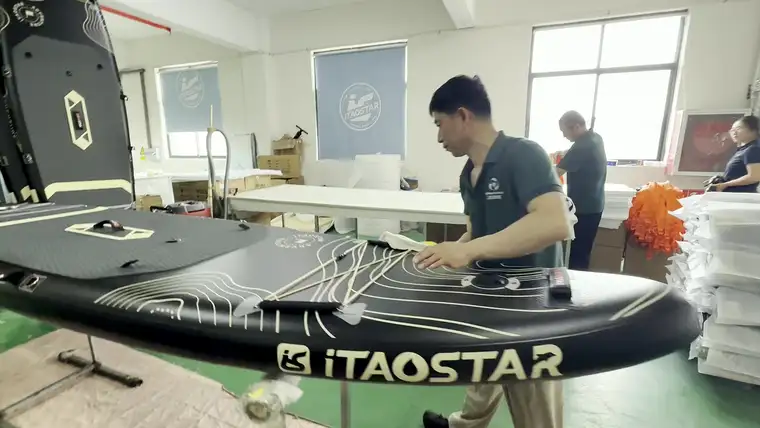
In the clean area, QA wipes deck, pad, fin box and rails with a residue-free cleaner before the board is signed off.
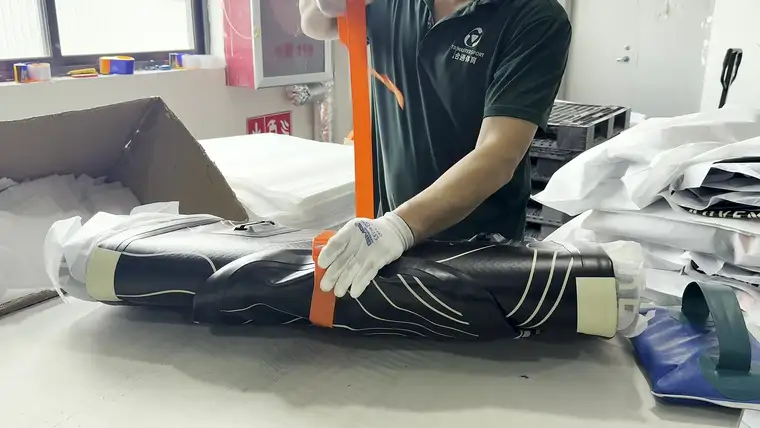
12 Station
Air is pulled out, foam goes on the fold points, and the board is rolled and strapped.
03Moving record
Edge buffing, pad glue, batch trimming and packing, each paused on its first frame until you press play.
04Details
Corner work, batch trimming and the pressure walk that closes a batch out.
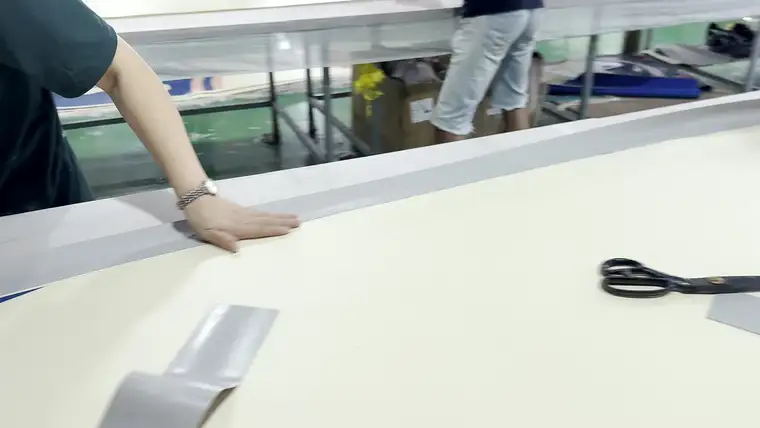
E01Rail alignment
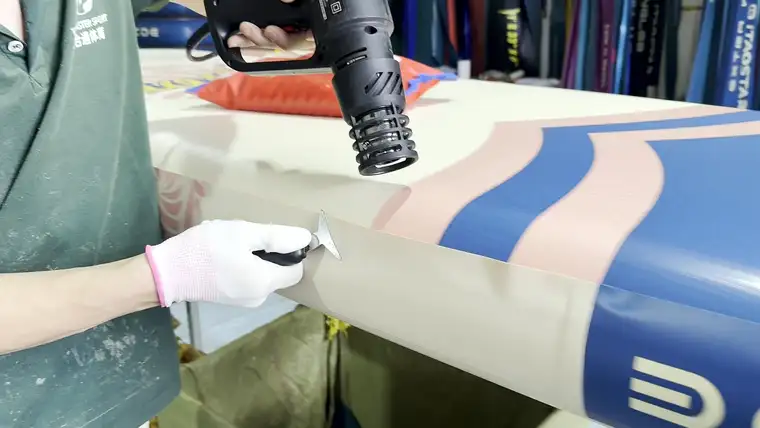
E02Outer rail close-up
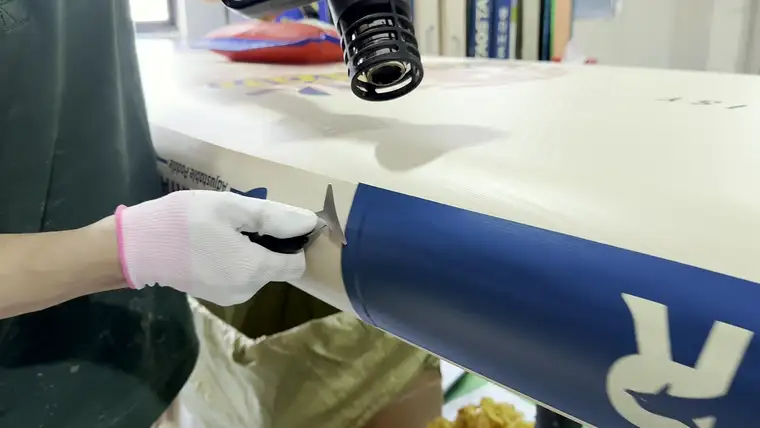
E03Corner detailing
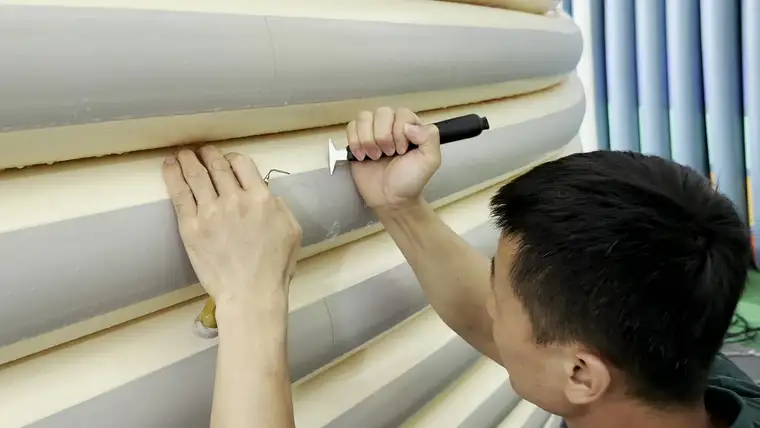
E04Batch trimming
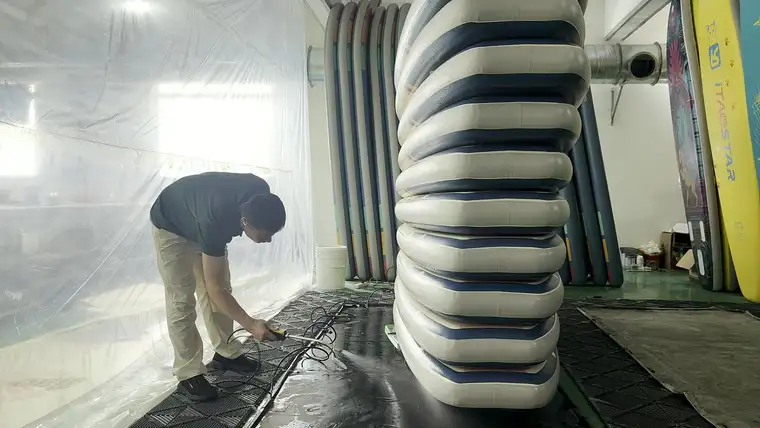
E05Stacked holding
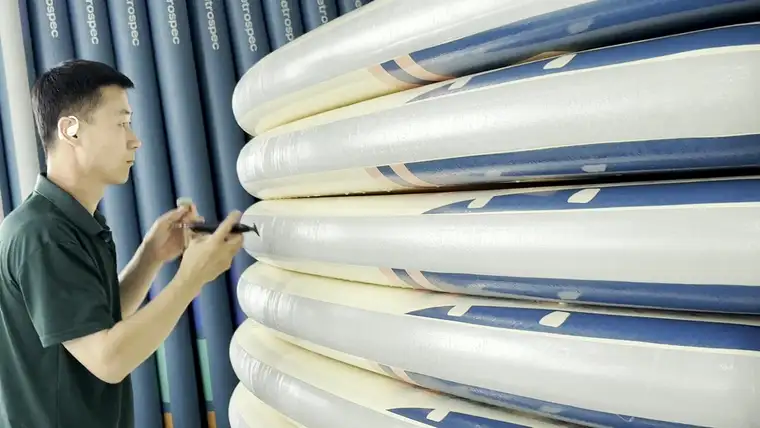
E06Pressure check
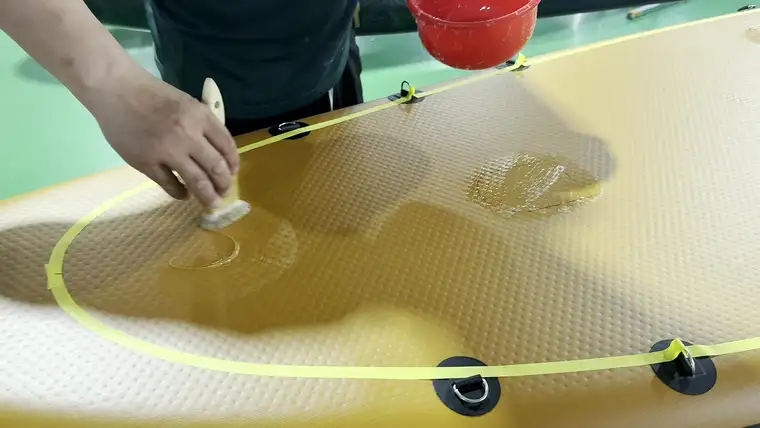
E07Masking
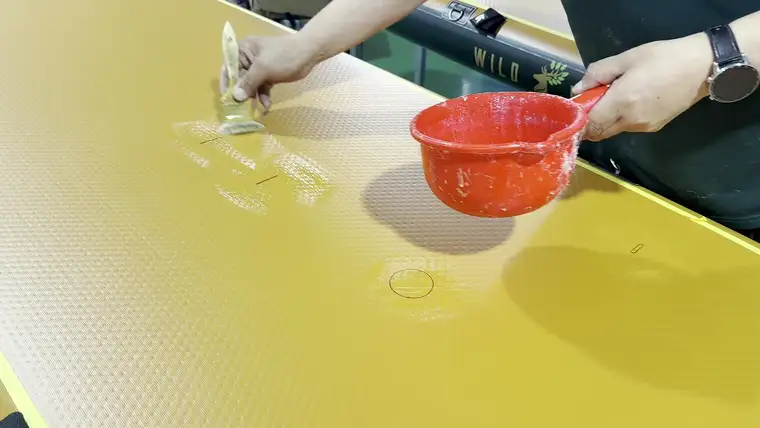
E08Handle and D-ring glue
E09Bagged and stacked
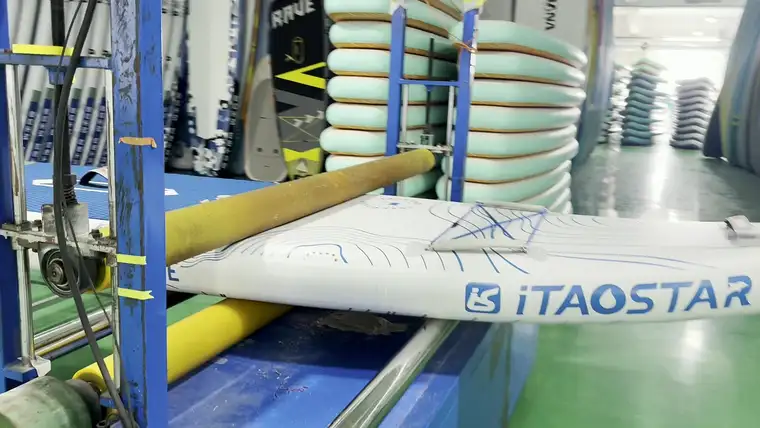
E10Roller line, wide